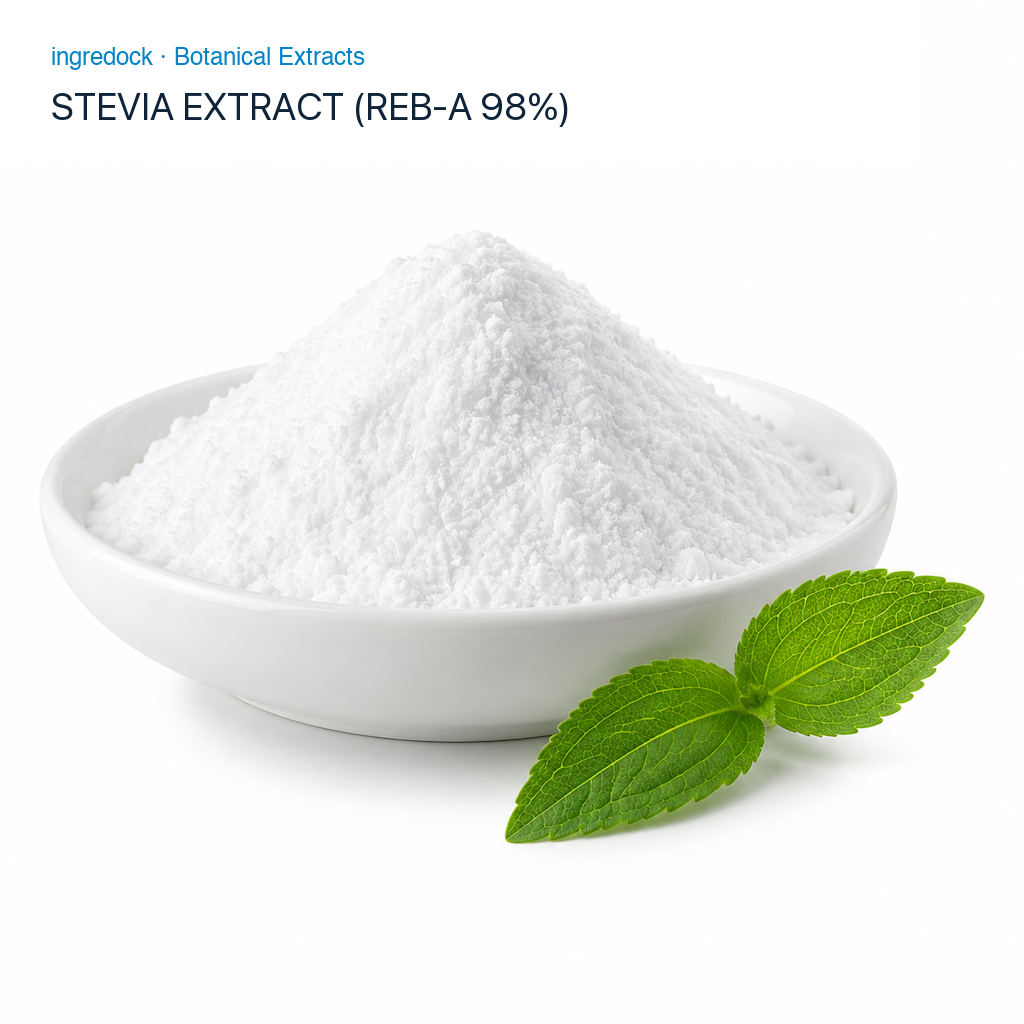
Ultra-purified zero-calorie natural stevia leaf glycoside extract. Reb-A 98% delivers ~350-400x sucrose sweetness with zero licorice aftertaste. Non-GMO, JECFA/FDA GRAS certified.
| Product Name | Stevia Leaf Extract Powder (Rebaudioside-A 98% HPLC) |
| Botanical Source | Stevia Rebaudiana Bertoni (Dried Stevia Leaf) |
| Active Ingredient | Rebaudioside-A ≥ 98.0% (HPLC), Total Steviol Glycosides ≥ 99.0% |
| Particle Mesh Size (Selected) | ≥ 95% pass 450 Mesh (< 32 μm ultra-fine) · Zero Aftertaste Premium |
| Appearance & Color | Pure White Fine Crystalline Powder (Intensely clean sweet taste) |
| Moisture & Ash | Loss on Drying ≤ 4.0%, Residue on Ignition ≤ 1.0% |
| Heavy Metals | Total Heavy Metals ≤ 10.0 ppm (Pb ≤ 1.0 ppm, As ≤ 0.5 ppm, Cd ≤ 0.5 ppm, Hg ≤ 0.05 ppm) |
| Solubility | 100% Freely soluble in water and ethanol; high pH (2-10) and thermal stability up to 200°C |
| Packaging Formats | 100g Sample Pouch, 1kg Vacuum Foil Bag, 20kg Standard Fiber Drum |
| Applications | Carbonated Drinks, Zero-Calorie Sweeteners, Protein Powders, Dairy, Confectionery, Tabletop |
Food Safety Management System
Hazard Analysis & Critical Control Points
Islamic Dietary & Purity Compliance
International Ecological Agriculture Standards
Independent Physical & Chemical Verification
Compliance Scope Notice: Certification documentation varies according to the specific botanical raw material, extraction ratio, and destination country. Lot-specific Certificates of Analysis (COA) are issued with every commercial dispatch.
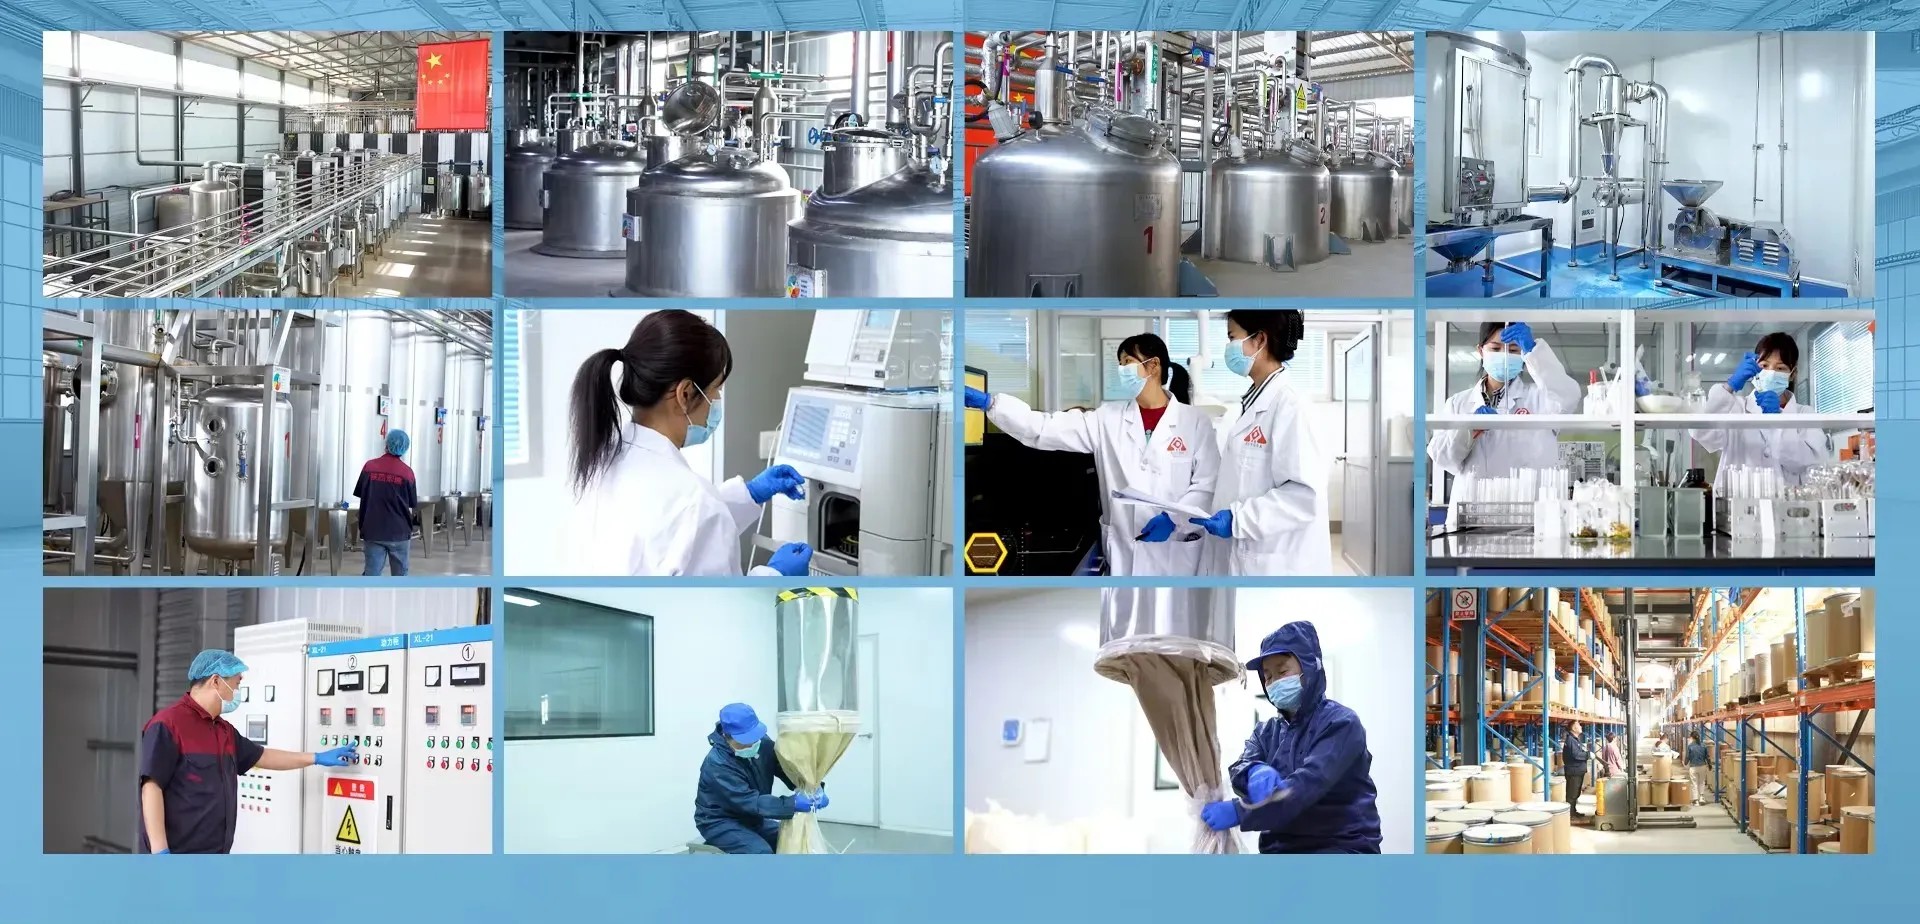
Through long-term audited partner production bases and partner GMP extraction facilities, we provide scalable botanical processing, analytical testing, and global export warehousing.
Our partner manufacturing bases operate multi-stage 316L stainless steel extraction tanks, low-temperature vacuum falling-film concentration, spray drying, and Class 100k cleanroom packaging.
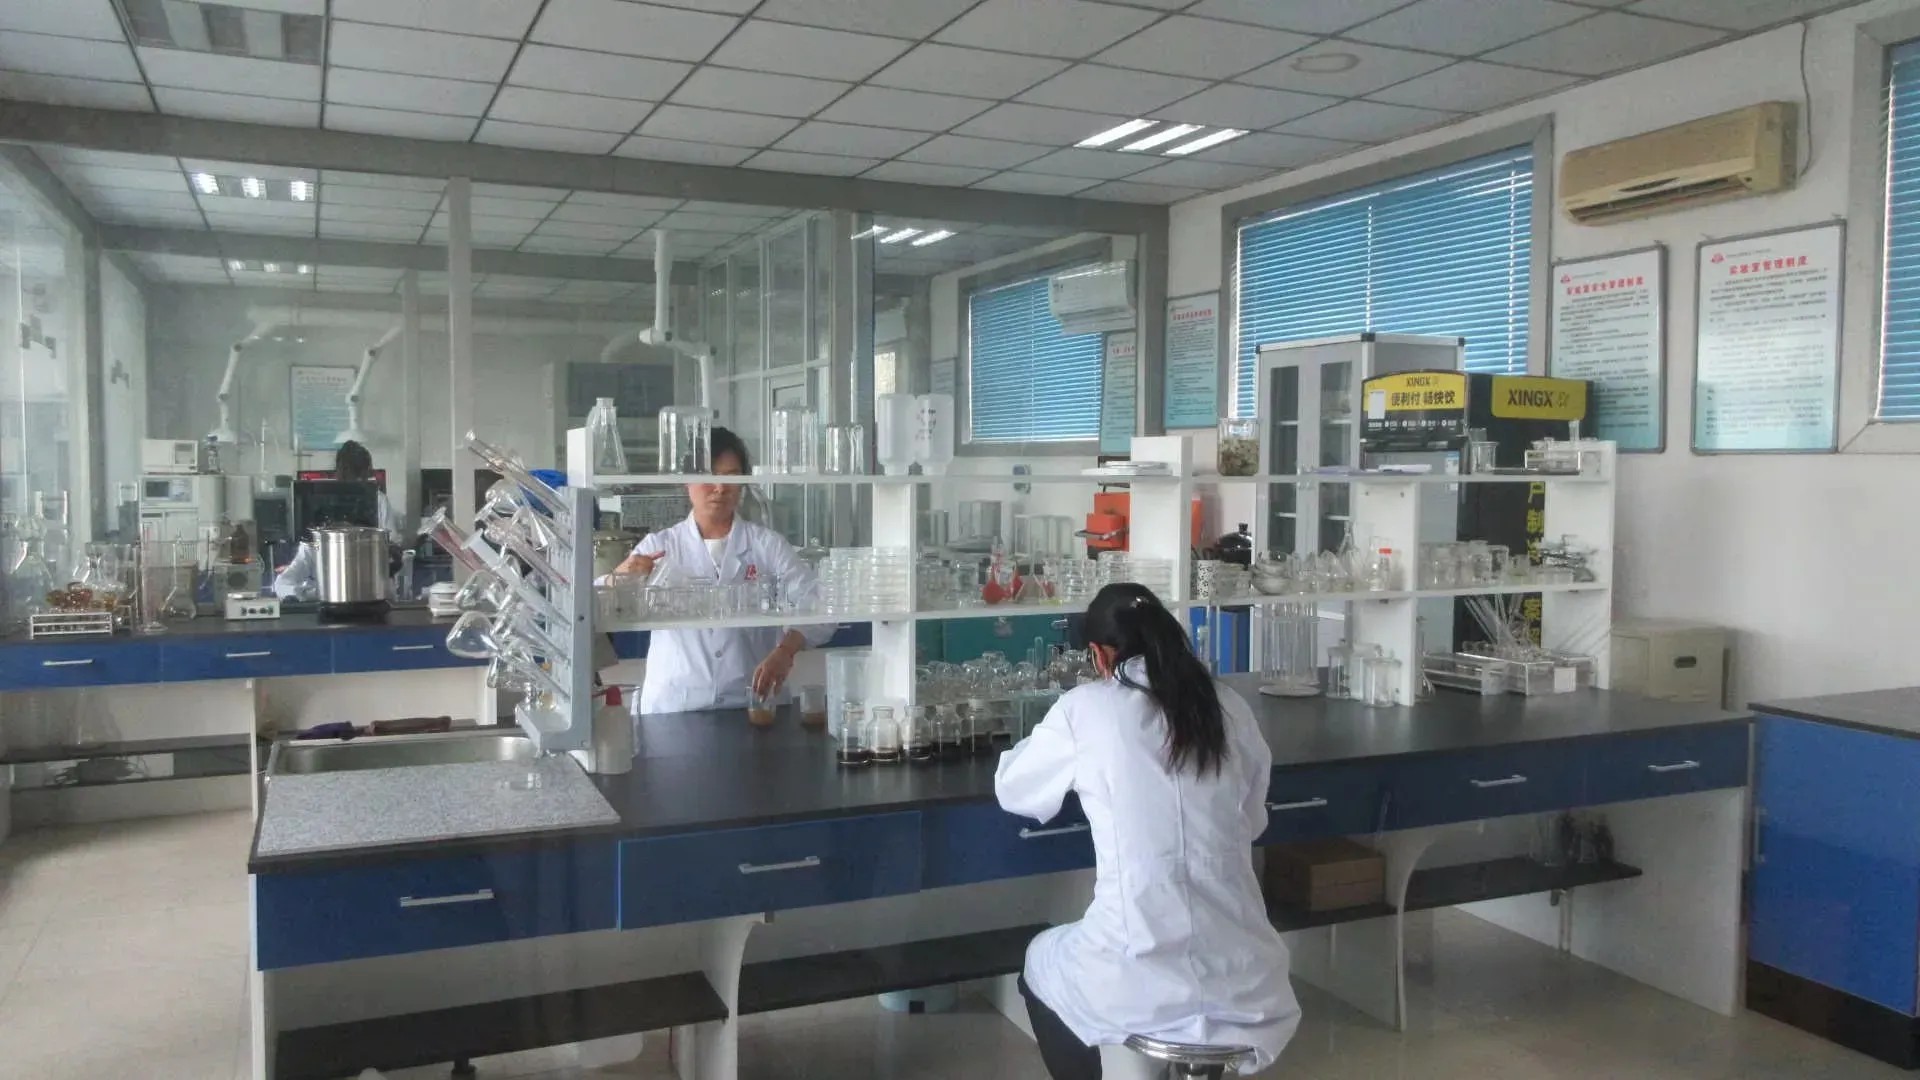
Associated testing laboratories conduct comprehensive HPLC, GC-MS, and microbiological release testing for every commercial lot.
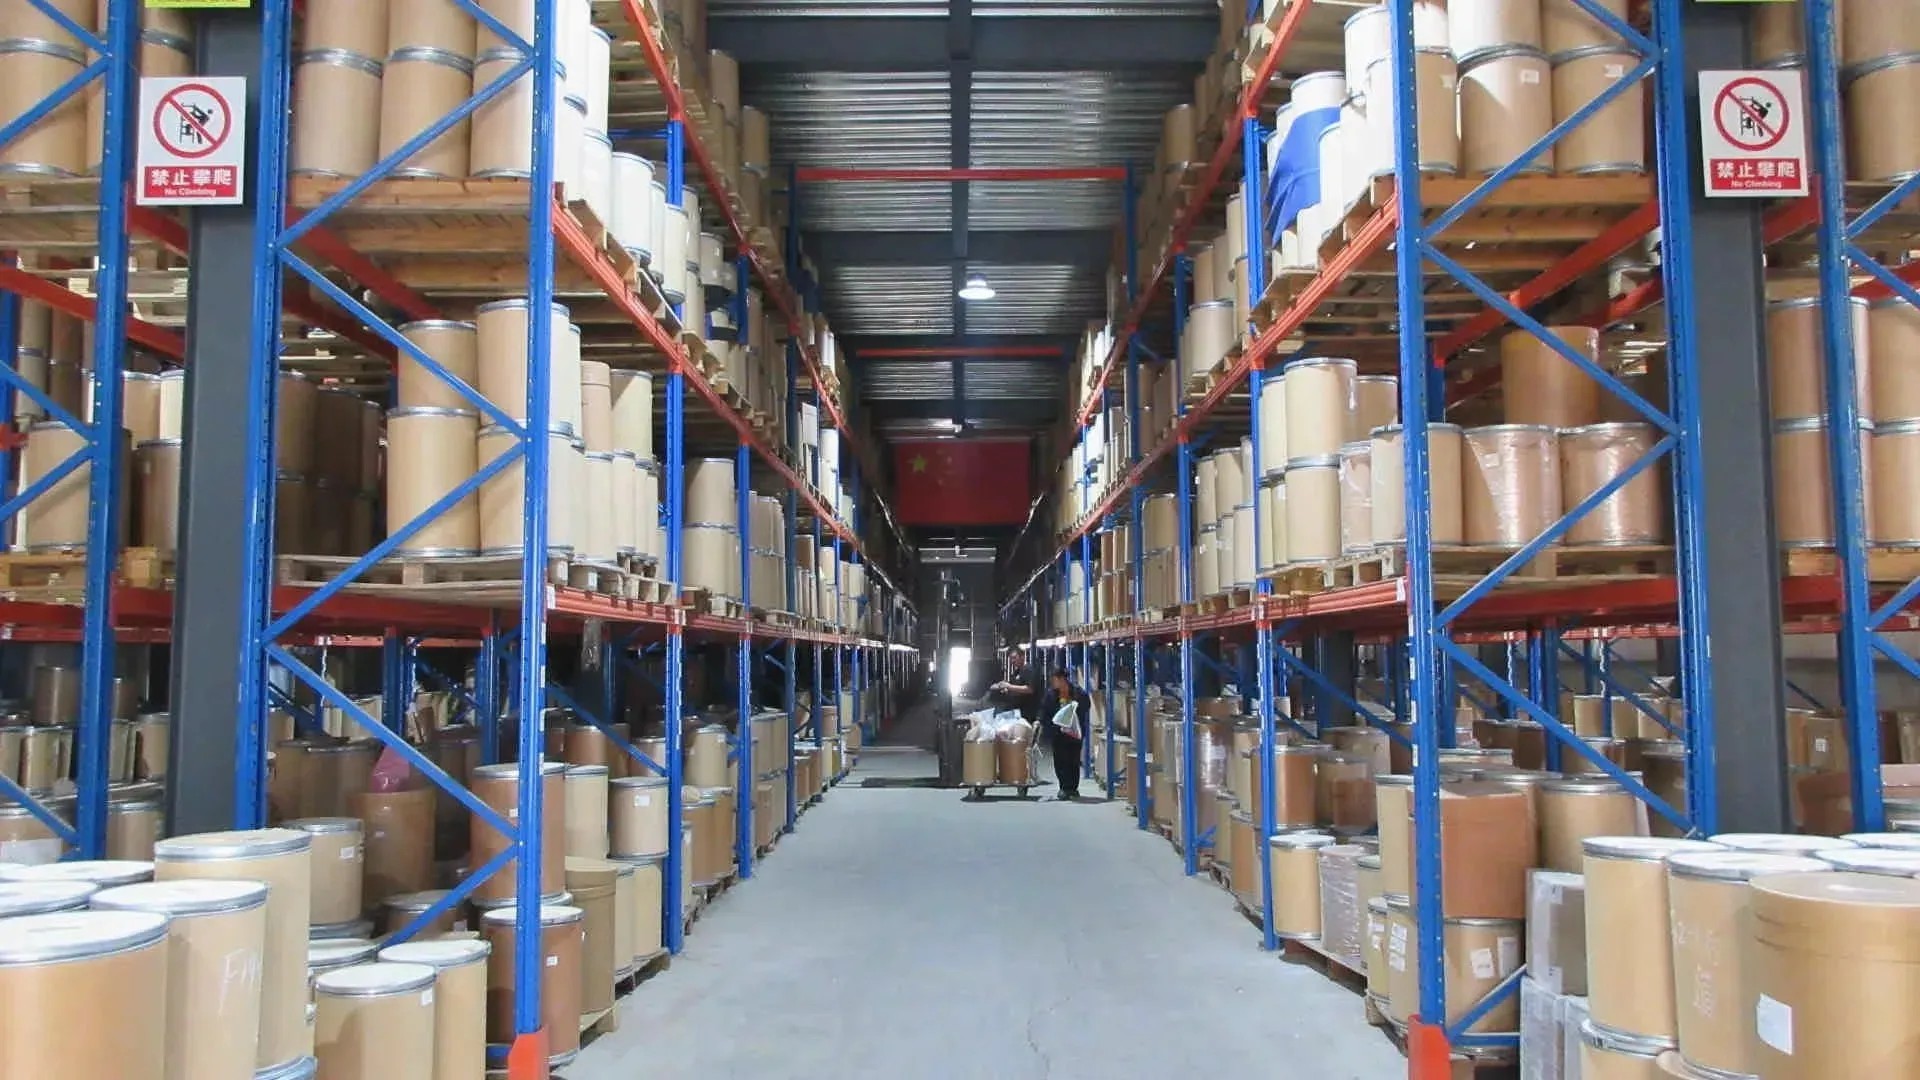
Partner temperature and humidity-controlled multi-tier racking warehouse ensuring export stability and palletized container transport.
Submit your inquiry below. Our commercial team will get back to your business email within 12 business hours.